Sub Zero Treatment
Sub Zero Treatment
Cryogenic Cooling to -80°C / -196°C for Dimensional Stability
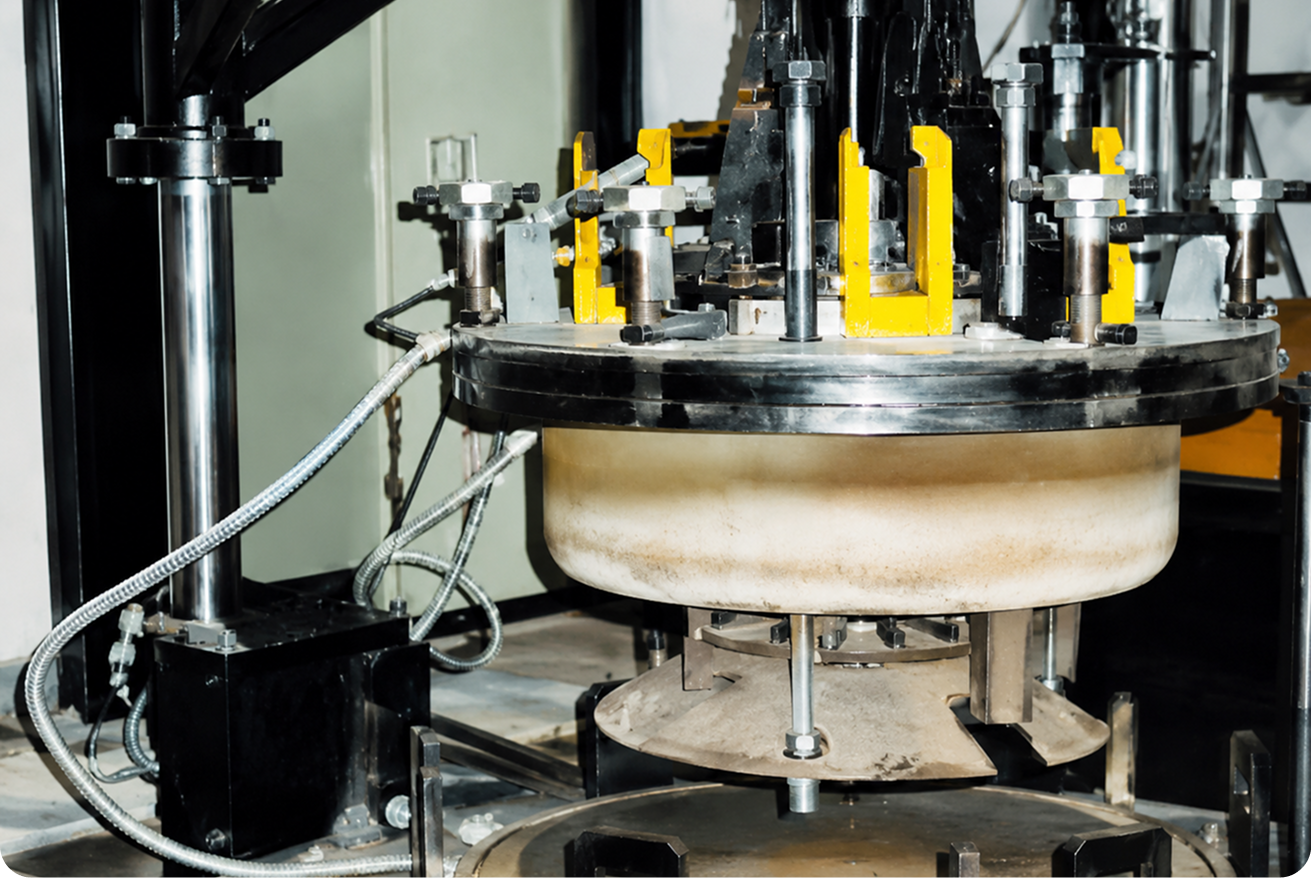
Sub zero and cryogenic treatment cools hardened tool steels and aerospace components down to sub-zero temperatures (-80°C in dry ice/chiller or -196°C in liquid nitrogen). This forces retained austenite to convert completely into martensite and precipitates ultra-fine eta-carbides.
Key Specifications
Eliminates Retained Austenite & Guarantees Zero Micron Drift
Retained austenite naturally decomposes over years into martensite, causing precision components to expand microscopically. Sub-zero processing eliminates this risk completely, making it mandatory for precision gauges, master bearings, and aerospace gyros.
Precision & Extreme Wear Applications
Used for aerospace bearings, gauge blocks, stamping dies, and cutting tools.
Slip Gauges & Calibration Masters
Zero micro-inch dimensional drift across lifetime calibration cycles.
Precision Plastic Mould Inserts
Optical mirror finish mould cavities with zero micro-shrinkage.
High-Speed Steel Cutting Endmills
M2/M35 endmills, taps, and broaches with 150-250% extended tool life.
Aerospace Precision Bearings
High-RPM jet engine bearings and satellite guidance actuators.
X-Ray Diffraction (XRD) Retained Austenite Audit
Quantitative Retained Austenite (RA%) verification using X-ray diffraction analysis at our partner NABL laboratory to certify sub-1% compliance.
Other Heat Treatment Services
Vacuum Hardening
Delivers bright, oxidation-free hardening with minimal distortion.
Gas Carburising
Enhances surface hardness while maintaining a tough core for improved durability.
Gas Nitriding
Produces a hard, wear-resistant surface without compromising core strength.